Māhikar
Manufacturing Protocol • Folio 04Lahore Manufacture

The Anatomy of Bespoke Manufacture

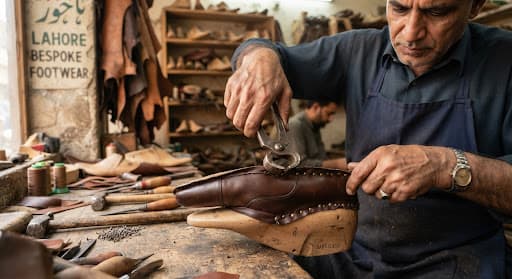
Inside our Lahore atelier, where multi-generational leather artisans cut, last, and welt footwear according to traditional European benchcraft standards.

Bench Capacity320 Pairs / MonthGuild Standard Tolerance
Last Turnaround21 Business DaysProto-Sample to Fit Approval

Sculpted Lasts

European hornbeam and seasoned beech blanks sculpted to bespoke foot profiles, graded with 1.2mm precision.

Hand-Sewn Welt

Artisanal 270° and 360° Goodyear storm and flat welting pitched with natural braided Irish flax.

Lahori Guild Lineage

Fourth-generation master clickers and bottom-makers blending historical Punjabi saddlery precision with British lasts.

European Tannages

100% full-traceability grain leather sourced directly from Annonay, Haas, Charles F. Stead, and J&FJ Baker.

The Chronology of Craft

The 8-Stage Bench Protocol

Every commission follows an uncompromising eight-tier sequence taking upwards of 36 bench hours. No pre-formed plastic components or synthetic fillers ever enter the manufacture floor.

  1. 01Foundation

    Carved Last Development & Grading

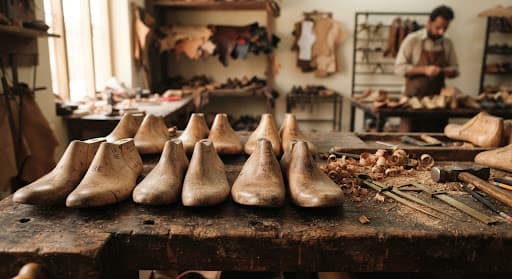
    The soul of the shoe resides in the wooden form. We carve initial master forms in hornbeam and beechwood, verifying arch pitch, instep girth, and toe box rake against client anthropometrics before digital grade-nesting into production sizing runs.

    • Hornbeam Blanks
    • Lateral Arch Support
    • Custom Pitch Angles
    Hand-carved hornbeam and beechwood shoe lasts arranged on a workbench beside brass calipers
    Stage 01 Specimen • Last AT-092 Chiselled Almond
  2. 02Material Sorting

    Full-Grain Leather Selection & Hand Clicking

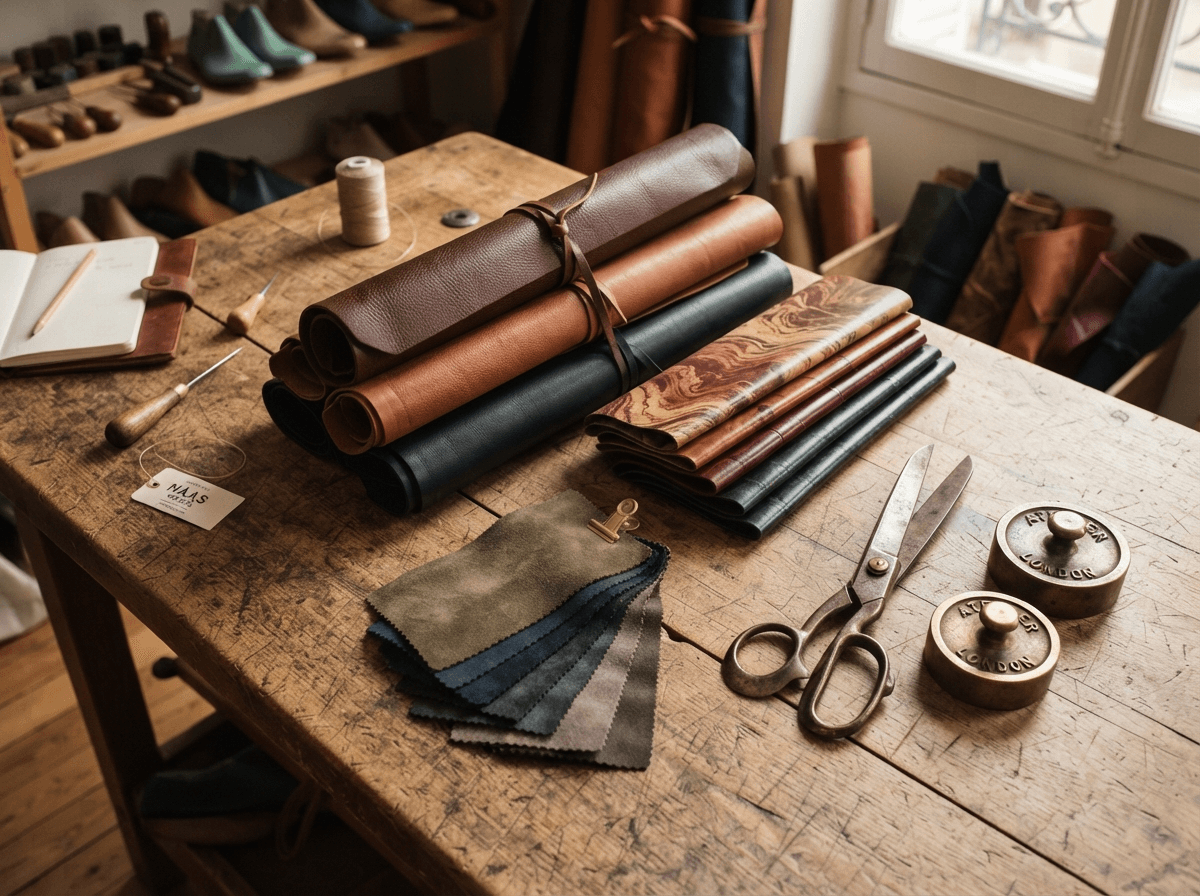
    Every hide exhibits directional stretch and natural tension lines. Our master clickers orient brass-weighted paper templates across the tightest center spine of the calfskin, discarding flank weaknesses to ensure left and right quarters mirror each other identically.

    • Spine-Aligned Cutting
    • Zero Flank Compromise
    • Full Grain Caliber
    Full-grain rolled leather hides, pattern shears, and swatch samples spread over a rustic timber worktable in Māhikar Atelier
    Stage 02 Specimen • Hand Clicking Table
  3. 03Prep & Joinery

    Upper Skiving, Folding & Precision Stitching

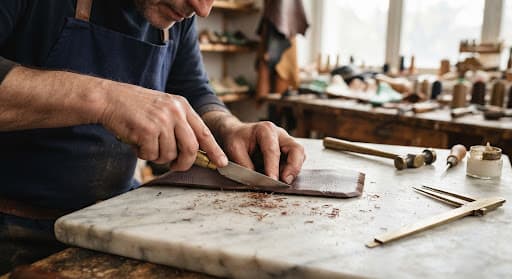
    Perimeters are hand-skived to a razor edge of 0.4mm, eliminating bulk where panels overlap. Edges are French-bound or carefully rolled with vegetable paste before dual-needle closing at 12 stitches per inch with bonded nylon thread.

    • 0.4mm Feather Skiving
    • 12 SPI Closing
    • French Binding
    Artisan hands thinning the margin of French box calf with a skiving knife on marble
    Stage 03 Specimen • Margin Bevel & Needle Tension
  4. 04Sculpting

    Hand-Lasting & Upper Conditioning

    The stitched upper is conditioned in steam chambers to activate the leather's natural pliability, then drafted over the last using lasting pincers. Pulled taut in eight micro-passes and tacked, the lasted upper rests for a minimum of 72 hours so memory locks permanently.

    • 72-Hour Last Rest
    • Pincer Drafting
    • Grain Moisture Retention
    Leather upper being drafted over a wooden last with lasting pincers and brass tacks
    Stage 04 Specimen • Drafting & Last Resting (72h)
  5. 05 • ARCHIVAL FOCUS

    The Goodyear Welt & Hand Stitching

    The defining signature of benchmade longevity. A 3.5mm thick vegetable-tanned leather welt strip is hand-stitched directly through the insole's carved holdfast feather using pitch-impregnated braided linen thread, creating an impenetrable water barrier while ensuring lifetime resolability.

    Thread Material
    Waxed Linen

    Braided flax soaked in pine rosin and beeswax.

    Insole Anchor
    Carved Feather

    Hand-channeled solid leather insole holdfast.

    Stitch Density
    10 SPI Density

    Evenly spaced with hand awl guide pricks.

    Welt Profile
    270° / 360° Options

    Flat welt, reverse storm welt, or Norwegian.

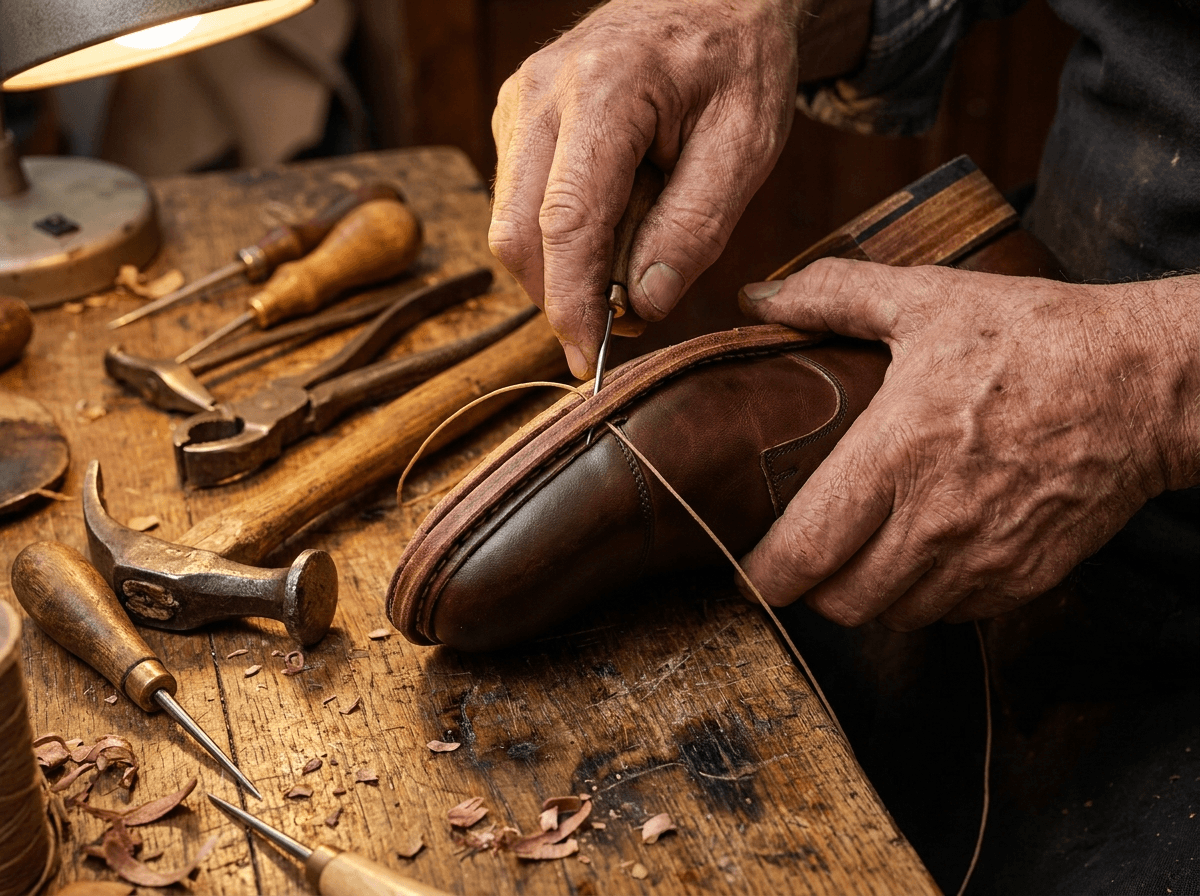
    Artisan shoemaker hands sewing the leather welt onto a dress shoe using a hand awl and waxed thread, workshop tools around on timber tableMaster Cobbler • Bench Station 02
    Macro Specification

    Hand-curved curved awl puncture passing through insole rib, upper edge, and exterior welt strip in a single continuous strike.

  6. 06Internal Architecture

    Natural Cork Filling & Spring Steel Shank

    The internal cavity between insole rib and outer welt is hot-filled with granulated natural Portuguese cork blended with pine pitch. A tempered Swedish spring steel shank is embedded to guarantee longitudinal arch support for the lifetime of the wearer.

    • Granulated Cork Bed
    • Tempered Steel Shank
    • Thermoreactive Cushion
    Granulated cork being pressed into the cavity of a welted sole with a steel shank at the arch
    Stage 06 Specimen • Cork Matrix Infill & Arch Anchor
  7. 07Sole Finishing

    Outsole Stitching & Sculpted Bevelled Waist

    The oak-bark sole is laminated under brass hydraulic press, then stitched with a concealed lockstitch through a closed cut flap. The waist is trimmed narrow and hand-sculpted into a fiddleback or round bevelled profile before heel block stacking.

    • Concealed Lockstitch
    • Bevelled Fiddleback
    • Stacked Leather Heel
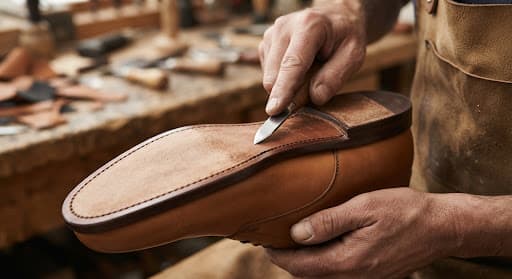
    Oak-bark outsole being bevelled along the waist with an edge shaping tool
    Stage 07 Specimen • Fiddleback Waist Sculpting
  8. 08Final Touch

    Hand Burnishing, Edge Ironing & Inspection

    Heel blocks and sole edges receive heated brass iron dressings with carnauba waxes. The uppers undergo multi-layer aniline glazing and hand-bone burnishing to achieve a deep mirror-like depth, followed by an exhaustive 42-point dimensional inspection.

    • Carnauba Hot Ironing
    • Mirror Glacé
    • 42-Point QC Gate
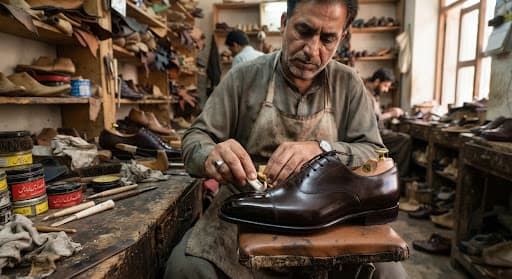
    Polisher applying wax to the toe cap of an espresso oxford to a mirror shine
    Stage 08 Specimen • Mirror Glacé & Archival Packing
Traceability & Tannages

Materials of Sovereign Caliber

We reject synthetic synthetics, corrected-grain skins, and rapid-tanned hides. Our partners represent historical European master tanneries with centuries of uninterrupted tradition.

100% REACH Compliant Tannages
FranceVocalou Box Calf

Tanneries d'Annonay & Haas

Full-grain French calfskin tanned using pure chromium salts and Alpine water. Delivers an extremely tight break, subtle oily temper, and resilience under repeated flexing.

Substance Caliber
1.2mm – 1.4mm Full Grain
ItalyRadica Museum Calf

Ilcea Tannery (Tuscany)

Hand-sponged marbled patina created with natural vegetable tannins. No two skins are identical, giving each pair an archival, museum-grade mottled depth.

Substance Caliber
1.3mm Marbled Grain
EnglandJanus & Superbuck

Charles F. Stead (Leeds)

World-renowned calf suedes treated with Scottish Scotchgard protection. Ultra-fine nap that does not mat, combined with exceptional tensile strength for unlined loafers.

Substance Caliber
1.4mm Heavy Nap Suede
England14-Month Oak Bark

J&FJ Baker Tannery (Colyton)

The oldest traditional oak bark tannery in the world. Hides pit-tanned for 14 continuous months in river water and English oak bark. Imparts legendary abrasion resistance.

Substance Caliber
5.5mm Heavy Insole/Outsole
B2B Institutional Solutions

Made to Order & Private-Label Precision

Each order is produced according to agreed client specifications, allowing international labels to create proprietary footwear lines without prohibitive tooling overheads.

We operate as the white-label manufacture engine behind bespoke tailoring houses in London, Milan, Tokyo, and Zurich. Our infrastructure accommodates both experimental limited-capsule runs and recurring seasonal store drops.

Institutional Sourcing Commitments

  • No Generic Tooling: Proprietary wooden and CAD lasts are stored in secure climate-controlled vaults under exclusive client NDA agreements.

  • True Goodyear / Hand-Welting: We do not offer cemented or Blake-rapid simulations disguised as welted shoes. All construction is structural.

  • Transparent Supply Chain: All hide batches accompany mill test certificates and import traceability manifests directly to your customs broker.

Private Label Capabilities Matrix

Specification Tiers

Debossed Insoles

Custom magnesium heat foil debossing with your house crest, archival typography, and internal serial numbering.

Branded Brass Soles

Flush-mounted brass toe plates, sunken logo rivets, and hot-stamped waist branding irons carved to your monogram.

Bespoke Patterns

Complete pattern generation from your physical vintage shoes, fashion illustrations, or tech-pack schematics.

Archival Packaging

Handmade rigid paperboard drawer boxes, unbleached heavy cotton dust bags, and brass-tipped travel shoe horns.

Flexible MOQs

Tiered order volumes starting at 12 pairs per silhouette for initial trials, scaling to 300+ pairs per collection drop.

Rapid Bench Prototyping

From CAD pattern to physical sample pair in 3 weeks.

Our dedicated sample cell allows designers, creative directors, and private labels to test last fits, leather hand-feel, and edge finishing with rapid turnaround before commissioning production batches.

Development SLA

FY 2025 Protocol
Phase 1: Last Profile & Spec Approval
Days 01–05
Phase 2: Hand Pattern & Clicking
Days 06–10
Phase 3: Goodyear Hand-Welting
Days 11–16
Phase 4: Finishing, Glacé & Courier
Days 17–21

Export Clearance: Air freight transit to UK, EU, UAE, & US within 72 hours via DHL Express Airway from Allama Iqbal International (LHE).